Pretoria, South Africa – September 28, 2026 – QILEE (Qilee Group), a global provider of integrated water treatment solutions with over 20 years of experience in industrial and municipal water management, has officially announced the launch of its new Containerized Modular Integrated Wastewater Treatment System. Unveiled in South Africa this September, the innovative system delivers a highly adaptable, rapid-deployment solution designed to address pressing water management challenges across industrial, municipal, and remote environments globally.
High Integration and Rapid Deployment
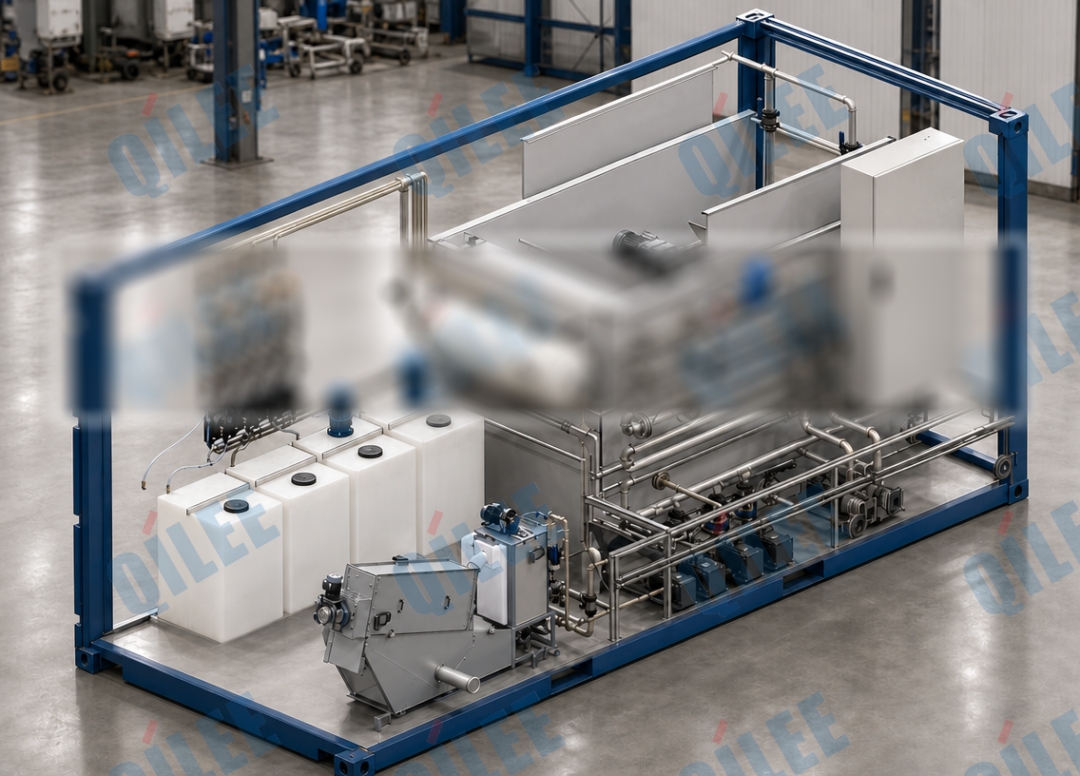
The newly launched system features a highly integrated, modular, and skid-mounted design. The equipment consolidates core wastewater treatment reaction units, chemical storage tanks, precise dosing systems, and essential pump mechanisms within a robust containerized steel base and supporting frame. This design includes all necessary pipelines, valves, air supply components, and advanced electrical control systems while deliberately reserving space for equipment inspection and maintenance.
By integrating these multiple functional units vertically and within a frame-based layout, the system maintains a highly compact footprint. This structure minimizes the need for dispersed on-site equipment installation and extensive civil construction work. A significant portion of assembly and factory testing is completed prior to delivery, ensuring convenient transportation. Once delivered to a project site, the equipment can be swiftly positioned, connected to utilities, and commissioned, making it uniquely suited for rapid-delivery applications and overseas projects.
Advanced Process Configuration and Automated Operation
Engineered for ultimate flexibility, the system can be customized based on specific treatment capacities, influent water quality, effluent standards, and required process configurations. A typical process flow incorporates influent pretreatment, precise coagulation and flocculation dosing, biochemical or physical-chemical reactions, solid-liquid separation, and final disinfection or advanced treatment for compliant discharge or reuse.
The system dramatically improves chemical dosing control by utilizing multiple storage tanks and metering dosing pumps to administer chemicals separately at distinct treatment stages, eliminating the instability and errors commonly associated with manual dosing. Depending on project specifications, the system can operate manually, semi-automatically, or fully automatically. Equipped with online instruments for monitoring liquid levels, flow rates, pressure, pH, and turbidity, the system enables coordinated control of pump sets and treatment units, significantly reducing the frequency of manual operation.
Diverse Target Markets and Global Applications
Designed to accommodate specific local discharge standards, climate conditions, and power supply capabilities, the Containerized Modular Integrated Wastewater Treatment System is highly targeted toward overseas markets requiring rapid deployment, particularly in Southeast Asia, the Middle East, and Africa.
The equipment provides targeted treatment solutions for factory production wastewater, domestic sewage, industrial parks, mining areas, and energy projects. Furthermore, it serves as an ideal decentralized wastewater treatment solution for remote locations, hotels, scenic camps, and temporary construction sites. It is also an effective tool for municipal authorities seeking emergency treatment, capacity expansion, or standards upgrading at existing facilities. QILEE notes that for industrial wastewater with high concentrations, strong corrosivity, or heavy metals, thorough water quality testing is conducted prior to equipment selection to ensure specialized pretreatment units are appropriately integrated.
Targeting environmental departments of industrial enterprises, EPC contractors, water service operators, developers, and overseas wastewater equipment distributors, the system offers an easy-to-expand structure where additional modules can be seamlessly added as project demands grow.
Comprehensive Production and Turnkey Delivery
QILEE ensures rigorous quality control through a standardized, multi-step production process. The lifecycle of each customized unit begins with precise project requirement confirmation and process design, followed by structural fabrication, equipment positioning, and meticulous piping and electrical control integration.
After comprehensive factory inspection and trial operations, the modular system is transported to the site for final installation. QILEE concludes the delivery process by conducting clean-water trial operations, water-flow commissioning, and verifying effluent compliance, alongside providing extensive operation and maintenance training for seamless customer handover.
About QILEE
QILEE (Qilee Group) is a leading global provider of integrated water treatment solutions, serving customers in more than 50 countries and regions. Specializing in high-efficiency sedimentation technology, membrane separation technology, and containerized mobile water treatment equipment, QILEE is committed to addressing global water scarcity challenges through innovative, reliable, and deployable technologies.
Learn more at: https://www.qileegroup.com/
Inquires can be sent to +86 13370035529 or email qilee@qileegroup.com
Address: No. 351 Wenqu Road, Fengxian District, Shanghai, China.
Media Contact
Company Name: Shanghai QILEE Environmental Protection Equipment Co., Ltd.
Contact Person: Tina
Email: Send Email
Phone: +86 13370035529
Country: China
Website: www.qileegroup.com